Custom Bakery Conveyor Systems
The Henry Group offers a wide array of bakery conveyors and conveyor systems for a broad range of applications. THG makes custom conveyors for bakeries for the most common applications to convey pans, peel boards, boxes, cartons, and baskets. We also offer product conveyors for raw, cooked, and finished goods in washdown or non-washdown designs. We custom design-build bakery conveyor systems to meet your specific needs. We make unique conveyors like reciprocating, indexing, sorting, merging, or vertical switch conveyors. We manufacture oven and Proofer Grouping and load-on conveyors as well as discharge conveyors that integrate with our Oven loaders and unloaders. We manufacture custom conveyors for almost every application and configuration for the wholesale bakery.
How Conveyors Connect the Line
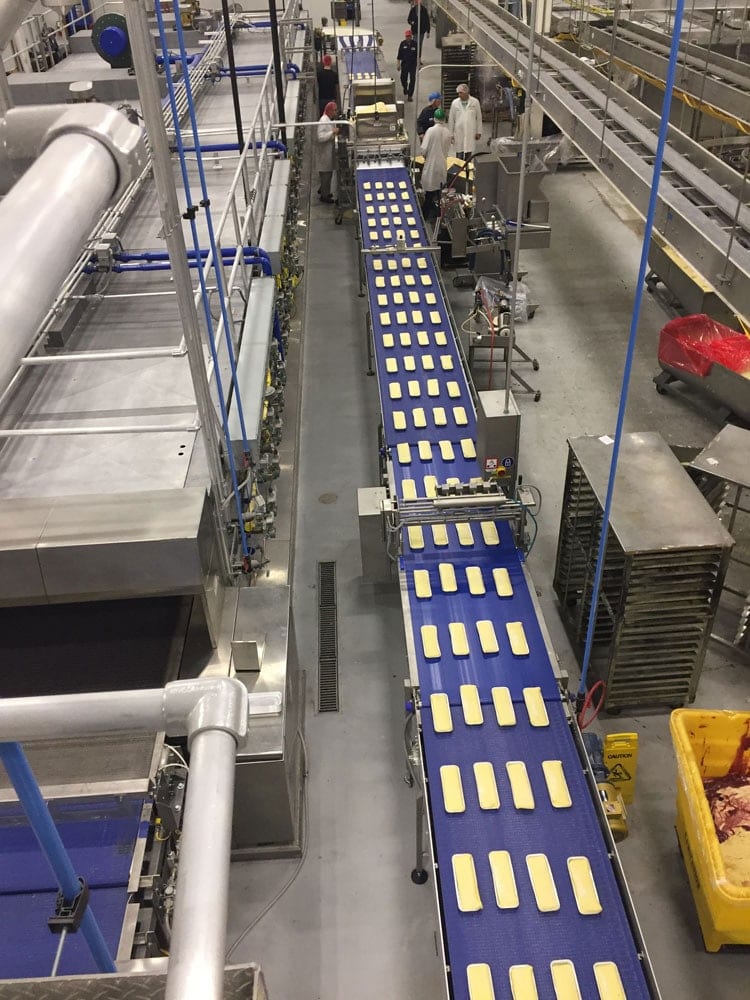
On a THG line, conveyors carry pans and product from one machine to the next at the rate the line runs. Grouping and load-on conveyors feed the proofer; after proofing, a grouper gathers pans into oven-sized groups for the oven loader; at the oven discharge, chain cross conveyors take pans away at a right angle; and from there conveyors carry product through cooling, depanning and pan cleaning to packaging such as bread baggers.
What THG Conveyors Carry
THG builds pan conveyors for bread, bun, sheet and specialty pans, including magnetic conveyors at pan cleaners and depanners; product conveyors for raw, baked and finished goods; and conveyors for peel boards, boxes, cartons and baskets. Where a line needs more than a straight run, THG builds reciprocating and indexing conveyors, sorting and merging conveyors that split or combine product flow, spreaders that set lane spacing, 90° curves, incline and decline conveyors, and vertical switches that change elevation.
Conveyors Supplied with THG Equipment
- Grouper and 90° transfer conveyors ahead of oven and proofer loaders
- Chain cross conveyors that discharge pans from oven unloaders
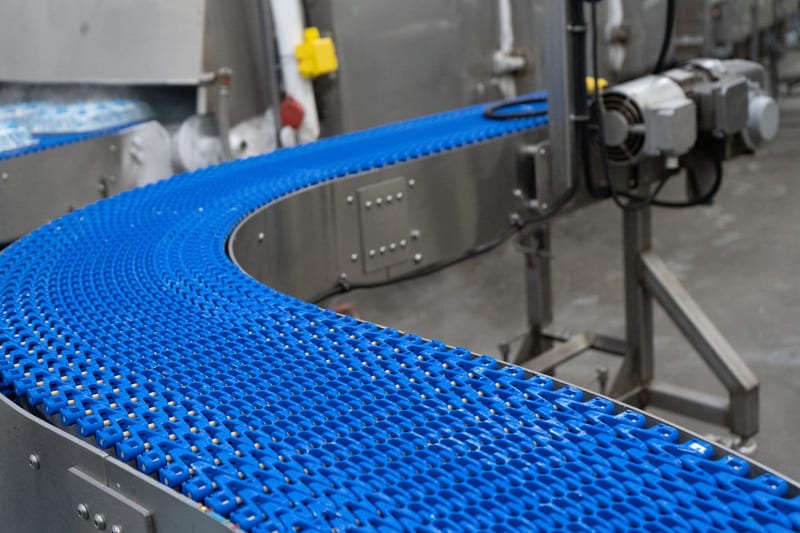
- 90° tight-radius curves with continuous modular belts
- Stainless spreader conveyors with lanes adjusted by hand crank
- Washdown incline and decline conveyors and vertical switches for spiral proofers
- Magnetic pan conveyors for pan cleaners and depanners
- Portable transfer conveyors on casters that roll away for sanitation
Built for Bakery Conditions
Product conveyors come in washdown or non-washdown designs, chosen for what they carry and how the area is cleaned. Portable transfer conveyors on casters roll away after production so sanitation crews can reach the rest of the line.
Configuration Options
- Modular plastic belts, chain conveyors or magnetic pan conveyors
- Widths and lengths built to suit the line and layout
- Speeds matched to the equipment on either side
- Interlocks with ovens, loaders and downstream equipment
- Washdown or non-washdown construction
Installation and Service
THG crews install conveyor systems on their own or as part of new lines, expansions and relocations. The Greenville fabrication facility has built conveyors to support THG's field installations since the 1980s. See equipment installation and replacement parts.
Common questions
Can you build conveyors to fit our existing equipment?
Yes. THG custom designs and builds conveyor systems for the layout and equipment you already have, including grouping, load-on and discharge conveyors for ovens and proofers.
Should our conveyors be washdown or non-washdown?
THG builds product conveyors for raw, baked and finished goods in either design. The choice depends on what the conveyor carries and how your sanitation crew cleans the area.
Do you install the conveyors?
Yes. Conveyor systems installation is one of THG's installation services, on its own or as part of a complete line installation or relocation.
Talk with THG about your equipment.
Share your product, the process and the equipment you need to connect.